XIAMEN ACEY NEW ENERGY TECHNOLOGY CO., LTD.

Categories
New Blog
How to Choose a Battery Pack Assembly Line: Semi-Automatic vs. Fully Automatic
November 04 , 2026Deciding between a semi-automatic and a fully automatic battery pack assembly line is usually the first real fork in any line project. The choice drives upfront cost, floor space, labor, changeover speed and how easily the line can grow later. This guide gives procurement and engineering teams a practical frame for choosing the right automation level before requesting quotations.
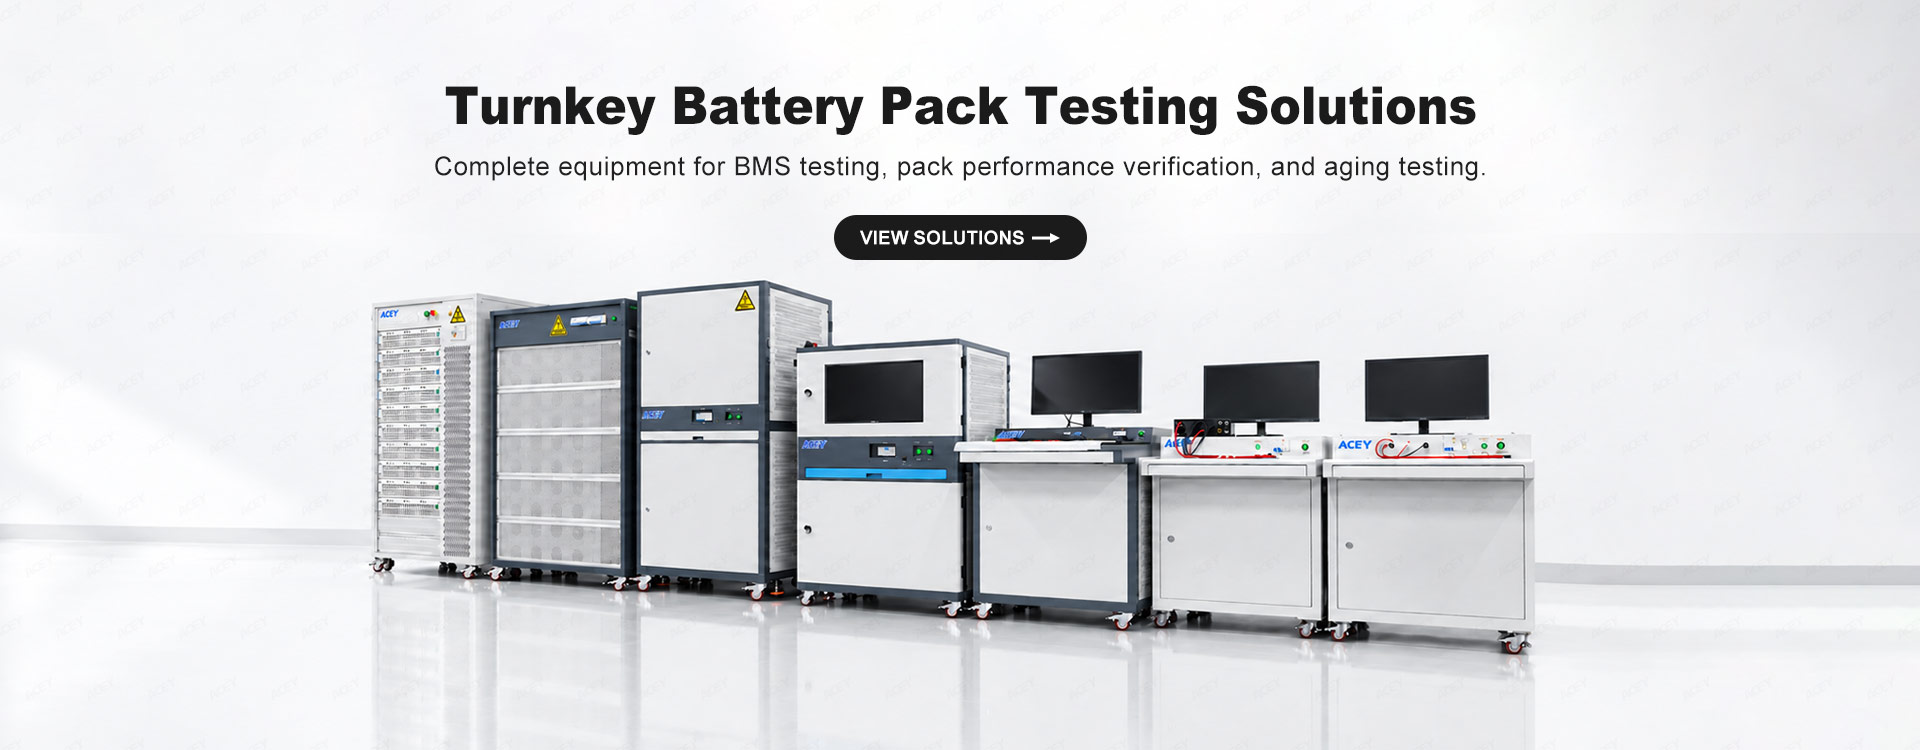
Before comparing brands or models, a buyer has to settle the automation level. A semi-automatic line and a fully automatic line are not the same product with different prices — they are different production systems. The semi-automatic version assumes operators move packs between stations, load fixtures and often perform manual steps; the fully automatic version moves packs on conveyors, performs stations with robots or dedicated machines, and logs data automatically.
Getting this wrong is expensive. Over-automating a low-volume, frequently-changing product wastes capital and complicates changeover. Under-automating a stable high-volume product caps output and ties up labor. The right answer depends on volume, product stability and how much engineering integration the factory can support.
A semi-automatic battery pack assembly line keeps the core process stations — cell sorting, welding, testing, inspection — but leans on operators for material handling and some manual operations. Typical characteristics:
Semi-automatic lines suit R&D, pilot runs, low or varied volume, and factories still learning their pack design. Upfront cost is lower and the risk of over-committing to one configuration is reduced.
A fully automatic battery pack assembly line connects stations with conveyors, transfers and a control system so packs move through the process with minimal operator touch. Typical characteristics:
Fully automatic lines suit stable, high-volume products where consistency, labor savings and data traceability matter more than frequent changeover. They require more engineering integration and a clearer, fixed product definition up front.
The table below compares the two levels across the factors that usually decide a project. Treat the descriptions as general guidance — actual capability depends on the specific line configuration and your pack design.
| Factor | Semi-automatic | Fully automatic |
|---|---|---|
| Operator involvement | High — loads, transfers and assists most steps | Low — automated transfer and handling |
| Throughput | Limited by operator pace and station balance | Set by station cycle time; sustained and repeatable |
| Changeover | Fast and low-cost; simpler fixtures | Slower; tooling and program changes needed |
| Upfront cost | Lower capital; easier to phase in | Higher capital and integration effort |
| Floor space | More space per unit output; spread stations | Compact, linear layout; less walking |
| Data & traceability | Partial; often manual records | Automatic logging, MES-ready |
| Best for | R&D, pilot, varied / low volume | Stable, high-volume production |
Volume is the single most useful input. A realistic packs-per-hour figure — under normal conditions and your actual pack topology — tells you how many stations you need and whether manual handling becomes the bottleneck.
The cell type changes how easily a line can be automated, because fixtures and joining methods differ by format:
If you run multiple formats, confirm whether one line can handle changeover or whether separate lines make more sense — format-specific tooling usually cannot be fully shared.
The purchase price is only part of the comparison. When scoping, also weigh:
Ask suppliers to state throughput, labor requirement and changeover time under the same defined pack specification, so proposals are comparable rather than optimistic.
Choose full automation when you have a stable pack design, sustained high volume, and a clear need for consistent cycle time, lower labor and automatic data traceability. If your product or volume is still changing, a semi-automatic or modular base is usually the safer start.
Often yes, if it is designed with standard interfaces and reserved space. Many factories start with semi-automatic sorting, welding and testing stations, then add automatic transfer, vision inspection and data capture as volume grows. Confirm upgrade paths with the supplier before ordering.
Yes. Cylindrical formats are generally the easiest to automate, prismatic scales well with compression and busbar welding stations, and pouch needs more custom fixturing. The core process stages are shared, but fixtures and handling differ by cell type.
Rm703, No.223, Qishan North Road, Huli District, Xiamen, Fujian, China
Email : allen@xmacey.com
Tel : +8618950009155
Whatsapp : +8618950009155